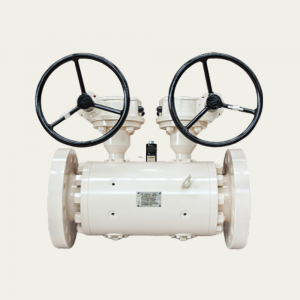
In the realm of industrial applications, the pursuit of efficiency is relentless. Stainless steel ball valves have emerged as a pivotal component in achieving optimal performance, owing to their robustness, durability, and reliability. Their capacity to handle high-pressure environments and corrosive substances makes them indispensable across various sectors, including oil and gas, chemical processing, and water treatment. As industries continue to demand higher standards of efficiency, understanding the role and benefits of stainless steel ball valves becomes essential. This article delves into how these valves enhance operational efficiency and offers insights into selecting the right valve for specific applications.
Understanding Stainless Steel Ball Valves
Stainless steel ball valves are engineered to provide a tight seal, ensuring minimal leakage and maintaining flow control. Their design features a spherical closure unit that can rotate to open or close the flow of liquid or gas. The material’s resistance to rust and corrosion enhances the valve’s longevity, making it suitable for rigorous industrial environments.
Key Features
- High Durability: Stainless steel construction ensures longevity and resistance to wear and tear.
- Corrosion Resistance: Suitable for corrosive environments, reducing maintenance needs.
- Temperature Tolerance: Capable of withstanding high temperatures, making them versatile for various applications.
- Pressure Handling: Designed to manage high-pressure systems effectively.
For a detailed understanding of these features, discover expert strategies here that highlight the engineering behind ball valves.
Advantages in Industrial Applications
The integration of stainless steel ball valves in industrial systems brings numerous advantages that contribute to enhanced operational efficiency:
- Reduced Maintenance Costs: The durability of stainless steel minimizes the frequency of replacements and repairs.
- Improved Safety: The ability to handle high pressure and corrosive materials reduces the risk of leaks and accidents.
- Efficient Flow Control: The design assures precise flow regulation, which is crucial for process optimization.
- Versatility: Applicable in diverse sectors, from food processing to petrochemical industries.
To explore the specific industrial uses and how they improve efficiency, learn about our tailored solutions.
Selecting the Right Stainless Steel Ball Valve
Choosing the appropriate stainless steel ball valve for a specific application involves several considerations:
Material Compatibility
Ensure the valve material is compatible with the substances it will handle to prevent corrosion and wear. Stainless steel is versatile, but it is crucial to verify its suitability for specific chemical interactions.
Pressure and Temperature Ratings
Understanding the system’s pressure and temperature requirements is vital. The valve must withstand these conditions to function effectively. Explore advanced guides and tips for selecting valves based on these parameters.
Size and Configuration
The size and configuration of the valve should match the pipeline specifications to ensure seamless integration. Consideration of the valve’s flow coefficient is also important for maintaining system efficiency.
For more detailed guidelines on selecting the right valve, find out more about this approach.
Conclusion
Stainless steel ball valves stand out as a critical component in enhancing industrial efficiency. Their robust design, coupled with superior performance in harsh environments, underscores their value in various applications. By carefully selecting and integrating the appropriate valve, industries can significantly improve operational efficiency, reduce downtime, and lower maintenance costs. Understanding the nuances of these valves allows for informed decision-making, ensuring that systems operate at peak performance. For further insights and expert recommendations, visit the comprehensive resources available at Flowlink EPL.